


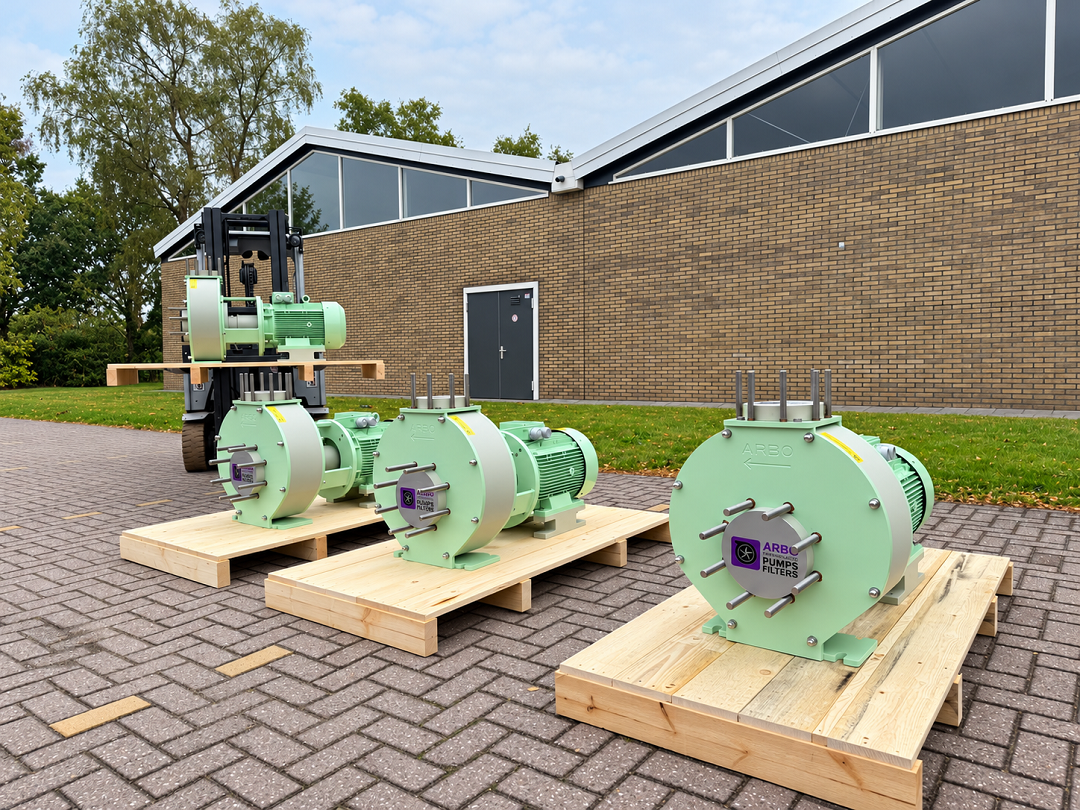
200,000 litres per hour. Per pump! Four impressive ARBO KR 125-250 pumps recently left our factory in Smilde, with GTL Europe in Venlo as their first destination. Their final destination? A new composting facility in China. An excellent example of an international project bringing together environmental technology, energy efficiency and reliable pumping solutions.
From composting to cleaner air
 Composting organic material generates process air containing ammonia and odorous compounds, among other substances. Treating this air is therefore an essential part of any composting facility.
A ventilation system directs the process air to an air scrubber, where it comes into contact with a specially formulated scrubbing liquid that captures ammonia and reduces odour emissions. Based in Venlo, GTL Europe develops and builds installations for the composting industry worldwide, combining expertise in the composting process with technical solutions for applications including process air treatment.
GTL has developed air scrubbers specifically for the composting industry, with technology that has proved itself in practice over many years. According to GTL, this technology can achieve ammonia reductions of up to 99%. The scrubber is therefore far more than just another piece of equipment. For the new project in China, GTL states that its use is even essential to obtaining the required permit.
And this is precisely where ARBO pumps come into play.
Four impressive pumps, each delivering 200,000 litres per hour
For this new project, ARBO supplied four KR 125-250 horizontal centrifugal pumps.
Each pump is designed to circulate as much as 200,000 litres of ammonium sulphate-containing scrubbing liquid per hour at a head of 7 metres. The pumps continuously recirculate the liquid within the air scrubber, enabling the process air to come into contact with the liquid needed to capture ammonia.
Alongside these large circulation pumps, the installations also use smaller pumps, including for draining scrubbing liquid from the system when required. Yet perhaps the most remarkable feature of the four large ARBO pumps is not their impressive capacity, but how they achieve it.
The power of 3D pump technology
Moving large volumes of liquid takes energy. Particularly in installations operating around the clock, pump energy consumption can make a significant contribution to total operating costs. That is why hydraulic efficiency was a key consideration in the development of our KR pumps.
The four pumps supplied incorporate ARBO’s 3D pump technology. The specific impeller geometry and pump casing design work together to provide exceptionally efficient liquid flow.
Equipped with six-pole electric motors, the pumps combine impressive flow capacity with low power consumption. With a pump efficiency of approximately 80%, our 3D pump technology demonstrates how large volumes of liquid can be moved efficiently while keeping energy consumption low.
The benefits of efficient hydraulic design are particularly evident in applications combining high flow rates with prolonged operating hours.
Put simply: pumping very large volumes of liquid without consuming unnecessary energy!
Resistant to aggressive liquids, built for continuous operation
 Beyond energy efficiency, air scrubber applications place another important demand on pumps: chemical resistance.
The scrubbing liquid used to capture ammonia can be chemically aggressive, placing considerable demands on pump materials. GTL therefore deliberately chooses ARBO’s plastic pumps. Their chemical resistance, low maintenance requirements and favourable energy performance make them particularly well suited to this application.
Operational reliability is equally important. Composting facilities must be able to operate 24 hours a day, seven days a week. Unplanned downtime is undesirable, so pumps need to be dependable and require as little maintenance as possible. According to GTL, end users generally keep spare parts and a standby pump available to help maintain continuity.
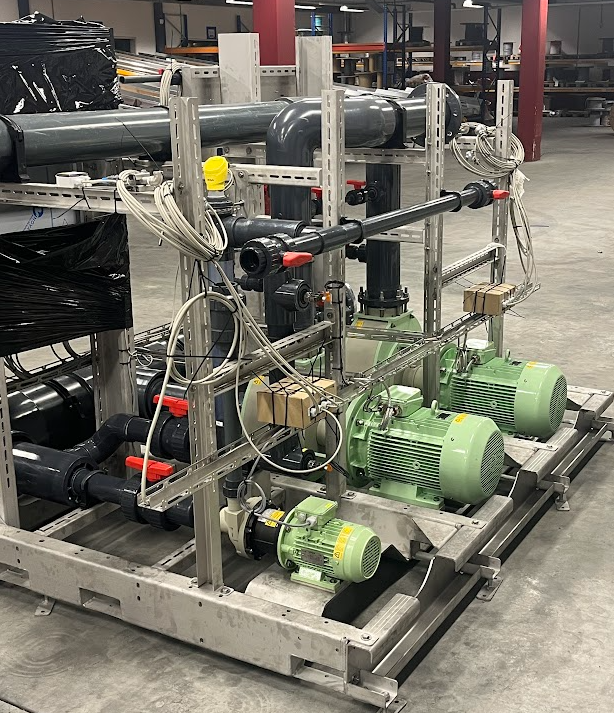
GTL also pays close attention to practical installation and assembly. In its air scrubber systems, pumps are integrated into pump skids: pre-assembled pumping units supplied on a plug-and-play basis. Once on site, they largely need only to be connected to become part of the complete system.
A smart solution that simplifies on-site installation.
Over a decade of working together in engineering
GTL Europe is far more than a supplier of composting facilities. With over 100 years of combined experience, more than 250 specialists and completed projects in 37 countries, the company has become an internationally active specialist in innovative, comprehensive technical solutions.
The partnership between GTL Europe and ARBO stretches back more than a decade. It is a longstanding, trusted relationship built on a shared practical approach, technical expertise and a commitment to quality and reliability.
While GTL develops and delivers complete composting facilities producing compost for mushroom cultivation, ARBO supplies the chemically resistant, energy-efficient pumping technology that plays a key role in those installations. The recent delivery of four large KR 125-250 pumps for the project in China is an excellent example.
But a successful partnership involves more than technology alone. GTL also values how ARBO operates as a supplier: commitments are honoured, quotations are followed up promptly and communication is straightforward. It is this combination of technical quality, mutual trust and a positive working relationship that has made our collaboration so rewarding over the years.
And that is something we are proud of!
Big pumps with an even bigger story
Four large pumps on wooden transport pallets. At first glance, simply another impressive delivery from our factory in Smilde. But there is a much bigger story behind these pumps.
It is a story of treating process air, reducing ammonia emissions, saving energy and keeping industrial installations running reliably on the other side of the world. At the same time, it is a story of two Dutch companies, each contributing its own specialist expertise to a smart technical solution.
From Smilde, via Venlo, to China. We have every reason to be proud!
Want to Know More?
Would you like to find out more about one of our products?
Contact the ARBO specialists for expert advice on capacity, material selection and configuration.
